Floor Level Palletizers: Key Solutions for Seamless Operations

In today’s fast-paced manufacturing environment, floor level palletizers are becoming a go-to solution for efficient, safe, and scalable packaging operations. As industries across India seek automation to streamline end-of-line processes, these systems provide the ideal blend of performance and cost-effectiveness.

In this blog, we explore what floor palletizing is, how it works, and why floor level palletizer machines are transforming packaging in industries like food, pharma, beverages, and more.

What Are Floor Level Palletizers and How Do They Work?

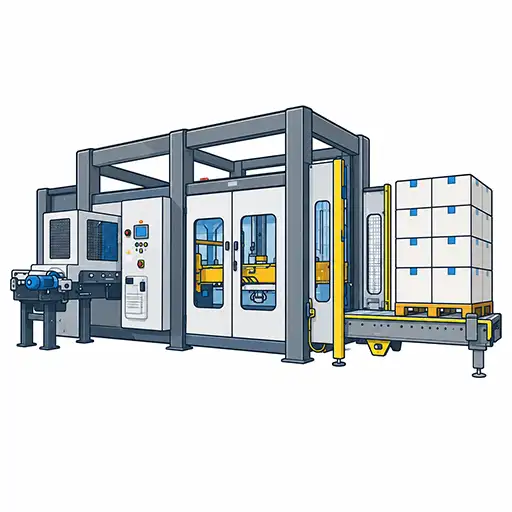
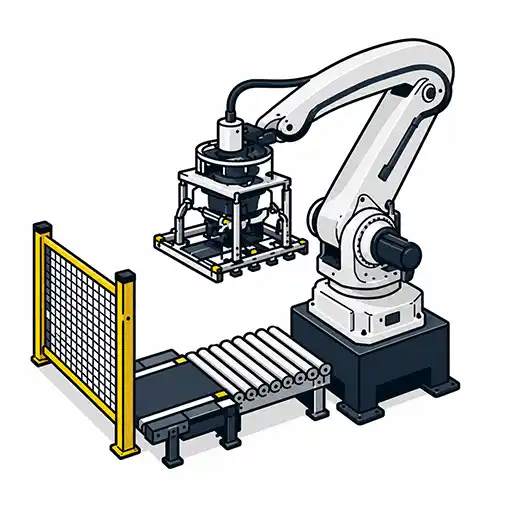
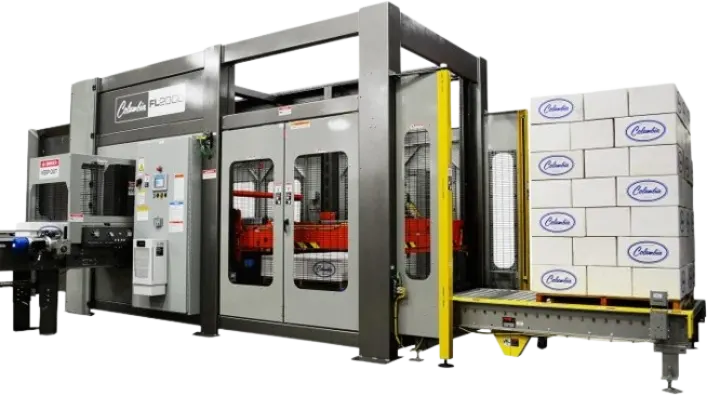
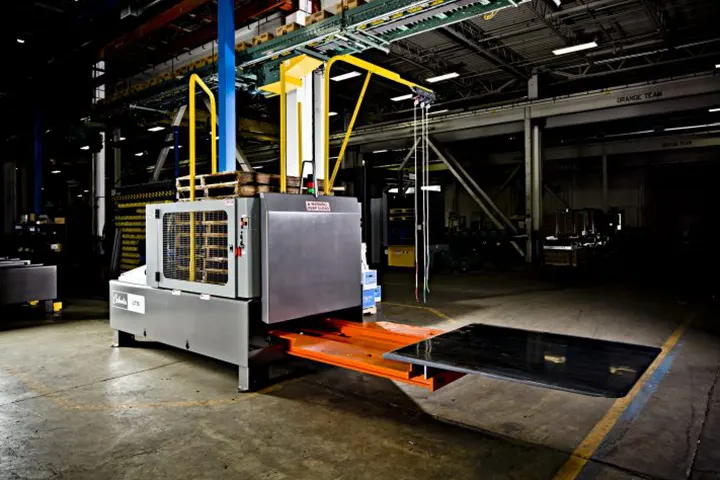
Floor palletizing solutions refer to systems that automatically stack products such as cartons, cases, or bags directly from the floor level eliminating the need for elevated platforms or mezzanines.

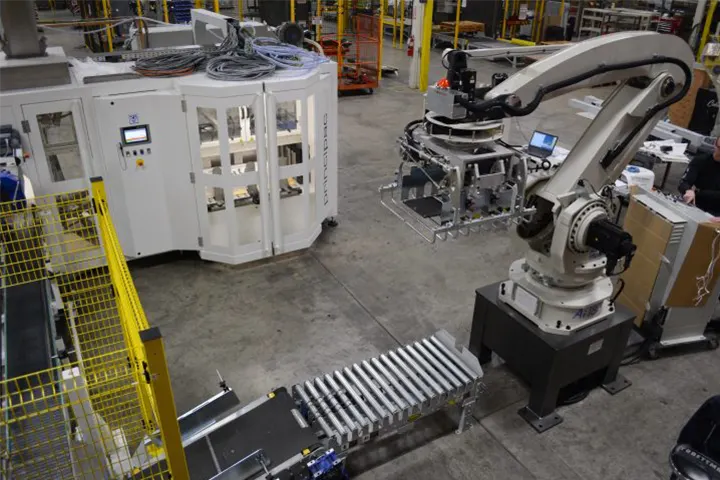
These systems work by receiving packages from a conveyor line, then using a combination of mechanical and sensors to place items in a pre-programmed pallet pattern. Once the pallet is full, it gets discharged automatically and a new one is positioned without manual intervention.

Floor palletizer machines offer seamless integration, versatile configuration options, and are a perfect fit for facilities aiming to adopt floor palletizing solutions at the end of the line—without the need for major infrastructure changes.

Key Benefits of Floor Level Palletizers for Indian Industries

India’s growing manufacturing sectors especially FMCG, Beverages, Dairy, Pharmaceuticals, Chemicals, Agro, and Retail require reliable palletizing solutions that can keep pace with volume while minimizing manual labor.

Here’s why floor palletizer machines are gaining traction:

  • Increased Throughput: Automates stacking at consistent speeds
  • Ease of Installation: No need for overhead conveyors or platforms
  • Lower Maintenance Costs: Simple design means fewer breakdowns
  • Reduced Labor Dependency: Streamlines repetitive tasks
  • Compact Footprint: Perfect for Indian factories with space constraints
  • Better Load Stability: Uniform pallet formation enhances transport safety

Floor Level Automatic Palletizing Machines: A Game Changer in the Packaging Industry

As automation continues to penetrate India’s mid- to large-scale factories, floor level automatic palletizing machines are becoming essential. These machines can handle 10–40 cases per minute, significantly improving production output while reducing downtime.

Whether integrated with case erectors, stretch wrappers, or labeling systems, these machines serve as the nucleus of modern packaging lines.

Floor Palletizing Solutions: Customizing to Meet Specific Needs

No two production lines are the same. That’s why floor palletizing solutions can be customized based on:

  • Product types (bags, boxes, trays, cartons)
  • Speed and throughput needs
  • Available floor space
  • Integration with existing conveyors or packaging equipment

At Columbia Machine India, we offer modular designs and custom end-effectors to deliver personalized solutions across various industrial needs.

Enhancing Food, Pharma, and Beverage Packaging in India

Indian industries are witnessing a transformation in their packaging processes. Floor level palletizer machines are playing a vital role in sectors such as:

  • Pharmaceuticals – Handling sensitive packaging with precision
  • Beverage – Speeding up bottling and crate palletizing
  • Food Processing – Maintaining hygiene standards while improving efficiency
  • Dairy – Managing crates and shrink-wrapped bundles effectively

These sectors benefit from increased automation, better traceability, and reduced product handling damage all made possible through intelligent floor-level palletizing systems.

The Role of Columbia Floor Level Palletizer Suppliers in India

Columbia Machine India brings global technology tailored to local requirements, offering:

  • In-house manufacturing
  • On-site installation and support
  • Industry-specific consultation
  • End-to-end project management

We help Indian businesses compete globally by offering robust, scalable, and efficient palletizing solutions.

What to Look for in a Floor Level Palletizer Machine Supplier

When selecting a supplier, consider:

  • Proven expertise in floor-level automation
  • Customization options
  • After-sales service and spare part support
  • Integration experience with existing systems
  • Proven case studies and references in your industry

Columbia Machine India checks all the boxes making us the preferred supplier of floor palletizer machines across the world.

FAQ

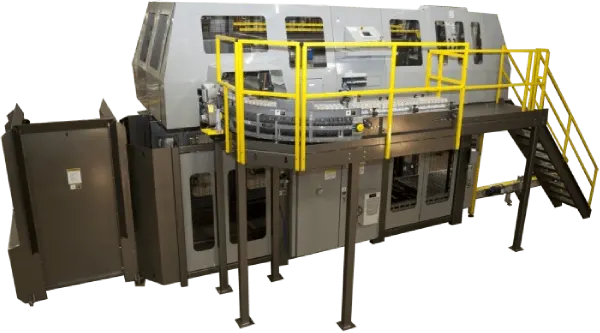
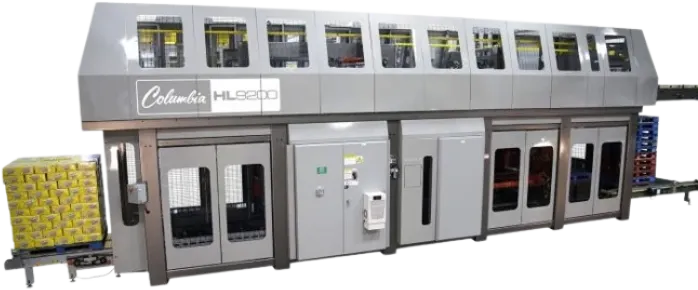
1. What is the difference between automatic and conventional high-level palletizers?

  • Conventional high-level palletizers are semi-automated and require more manual usage, whereas automatic high-level palletizers are completely automatic and employ less human intervention.

2. What industries benefit the most from high-level palletizers?

  • High-level palletizers come of great use in those industries requiring instant and effectual packaging solutions, for example, food and beverage, logistics, medicines, and consumer goods.

3. How much does a high-level palletizer actually cost?

  • The price of a high-level palletizer is actually based on factors like machine type, capacity, customization, and even brand. Automatic systems are a bit pricey compared to traditional ones, but they promise to provide better output.

4.Where can I find high-level palletizers for sale in India?

  • One can easily find high- level palletizers for sale with help from top manufacturers and suppliers in India. Many suppliers provide customized solutions for industries offering supreme quality, dependable palletizing tools.

5. How to select the correct high-level palletizer for my company?

  • While choosing the ideal high-level palletizer for your business, you should take into consideration factors like manufacturing volume, kind of product, customization needs, space needs, and after-sales help.
Copy link
Please enable JavaScript in your browser to complete this form.