High-Performance Floor Level Palletizer for Precision & Efficiency

Built for high-speed industrial environments, Columbia Machine India’s advanced Floor Level Palletizer systems deliver exceptional load stability, operational flexibility, and long-term production reliability while minimizing manual intervention and floor space requirements.

cases per hour
0 +
Max Payload
0 kg
System Uptime
0 %

Overview of Floor Level Palletizer Machines

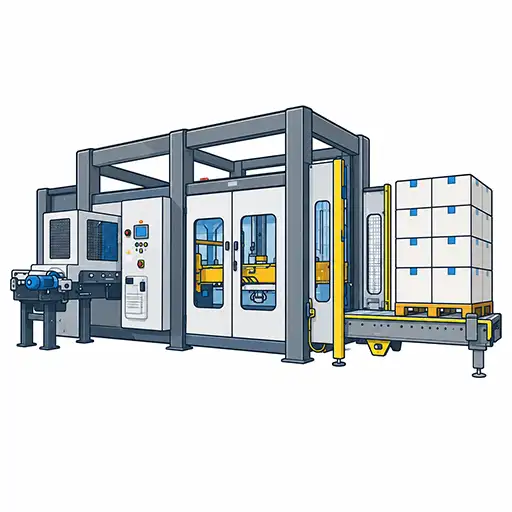
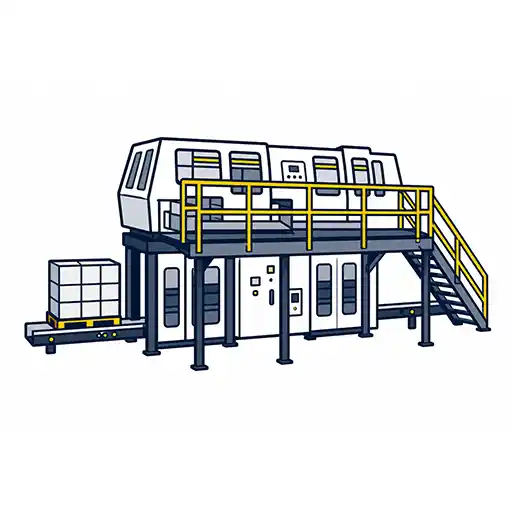
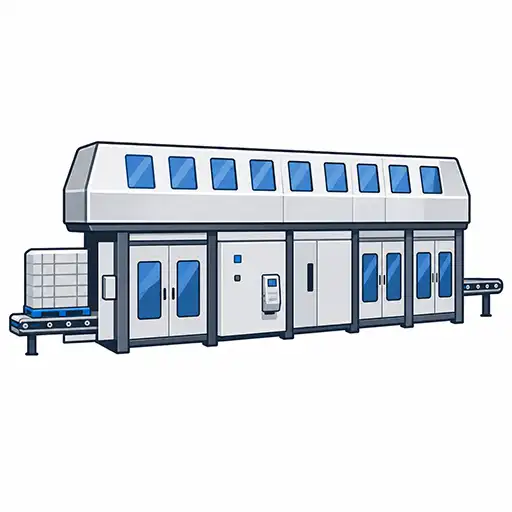
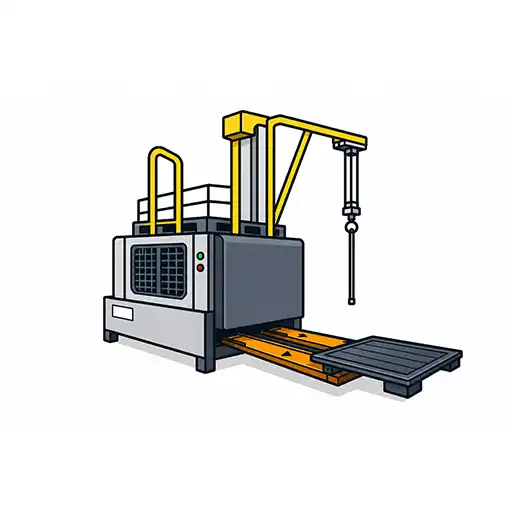
A Floor Level Palletizer is a fully automated palletizing solution engineered to receive, arrange, and stack products directly from ground-level infeed conveyors onto pallets with maximum efficiency and precision. Unlike elevated palletizing systems, floor-level configurations eliminate the need for mezzanines, structural platforms, or complex elevation systems, making them an ideal solution for facilities seeking simplified integration and optimized production flow.
As a leading floor level palletizer manufacturer in India, Columbia Machine India designs robust palletizing systems that support high-speed case handling, multi-format product compatibility, and effortless production line integration. Our systems are engineered for continuous industrial operations across FMCG, food processing, beverage, chemicals, logistics, personal care, pharmaceutical, and warehousing industries. The advanced architecture of our floor level palletizing system combines intelligent layer formation technology, servo-controlled movement, precision product orientation, and high-speed load transfer capabilities to deliver stable and repeatable pallet loads even under demanding production conditions.

QUESTIONS? CALL +91 72289 31741

imgi_4_FL1000-SW-7-scaled-1
FL1000-Hero-2-scaled-1-768x512
FL

What is a Floor Level Palletizer?

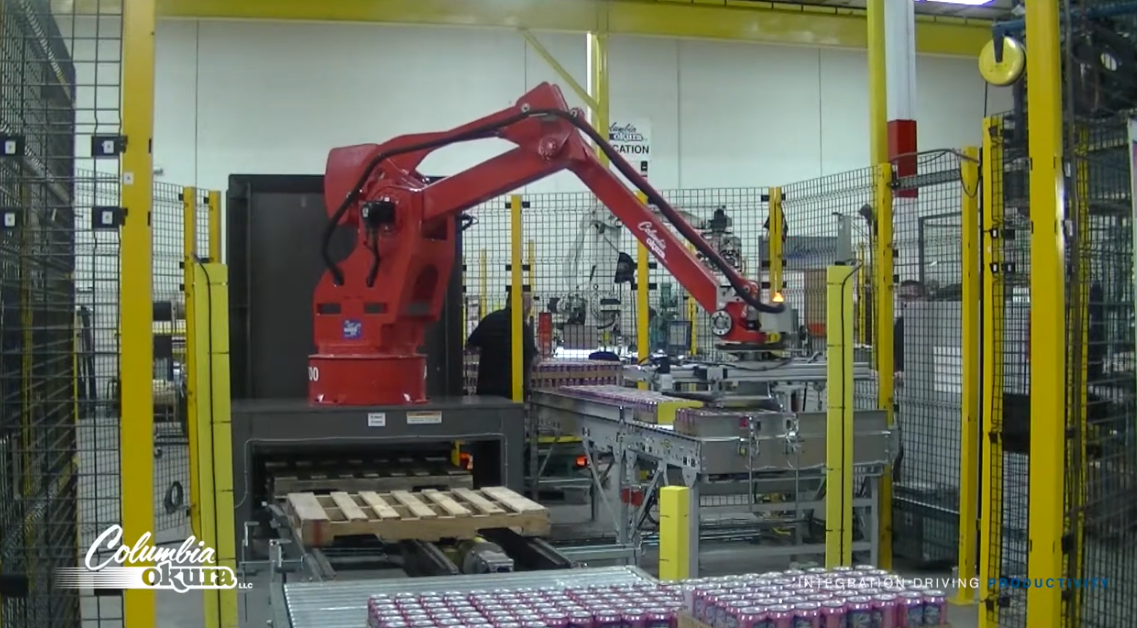
A floor level palletizer machine is an automated palletizing system designed to form organized product layers and transfer them onto pallets at floor height. Products enter through conveyor systems, are oriented into predefined patterns, grouped into layers, and stacked systematically using advanced mechanical and control technologies.

Compact Design

Operator Friendly

Easy Maintenance

Flexible Layout

Efficient Stacking

Cost-Effective Solution

QUESTIONS? CALL +91 72289 31741

Servo-Controlled Product Handling

Integrated servo motion technology ensures smooth product movement, reduced package damage, and accurate positioning.

PLC-Based Automation Controls

Industrial-grade PLC controls with Ethernet-enabled communication support Industry 4.0-ready automation, enabling real-time production monitoring, remote diagnostics, and with upstream and downstream equipment.

Flexible Packaging Compatibility

The system handles cartons, crates, bags, shrink-wrapped bundles, trays, pails, and multiple secondary packaging formats efficiently

Advanced Safety & Easy Integration

Equipped with Category 3 safety systems and designed for seamless integration with existing production lines.

Why Floor Level Palletizers Are Essential for Modern Manufacturing

The engineering design of Columbia Machine India’s automatic floor-level palletizer is optimized for high-throughput manufacturing environments, supporting palletizing speeds of up to 25 cases per minute while minimizing downtime and maximizing operational efficiency.

Heavy-Duty Structural Construction

Manufactured using industrial-grade fabricated steel frames for vibration resistance and long-term operational durability.

Modular Machine Configuration

Supports flexible layout customization based on production capacity, line direction, and available floor space.

Smart Product Alignment Technology

Centering guides and smart sequence systems maintain accurate product positioning during layer formation.

Integrated Pallet Dispenser

Fully automatic pallet dispensing systems reduce manual pallet handling and improve operational efficiency.

Advanced Safety Systems

Equipped with Category 3 electrical safety circuits, safety interlocks, guarded access doors, and emergency stop systems.

Maintenance-Friendly Design

Ground-level operation provides simplified machine accessibility for inspection, maintenance, and servicing activities.

Key Benefits of Floor Level Palletizing Systems

An automatic floor level palletizer that is carefully designed will offer the best mix of productivity, versatility, and operational value over time for today’s manufacturing environment.

Ethernet-Enabled PLC Controls

Integrated PLC systems support remote diagnostics, machine communication, and production monitoring.

Touchscreen Human Machine Interface (HMI)

Operator-friendly touchscreen controls allow quick pattern selection, fault diagnostics, and production parameter adjustments.

Unlimited Pallet Pattern Capability

Supports customized pallet stacking configurations for multiple product dimensions and packaging types.

Soft Product Turning Technology

Advanced turning systems protect delicate products during orientation and pallet formation.

Automatic Slip Sheet & Tie Sheet Integration

Optional dispensing systems improve pallet stability during transportation and storage.

Upstream & Downstream Conveyor Integration

The floor level palletizing system integrates seamlessly with existing conveyor systems, wrappers, barcode scanners, and warehouse automation equipment

Types of Floor Level Palletizers

We offer a wide variety of floor level palletizer machines that can be customized to meet different production capacities, layouts, and even specific demands of industries, so that they can deliver the best possible performance for each application.
1

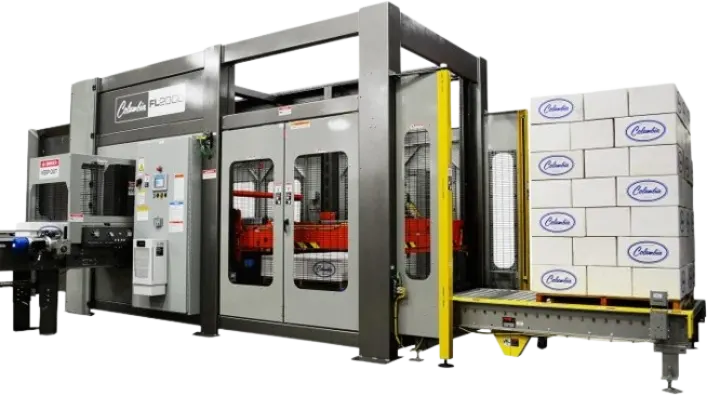
FL1000

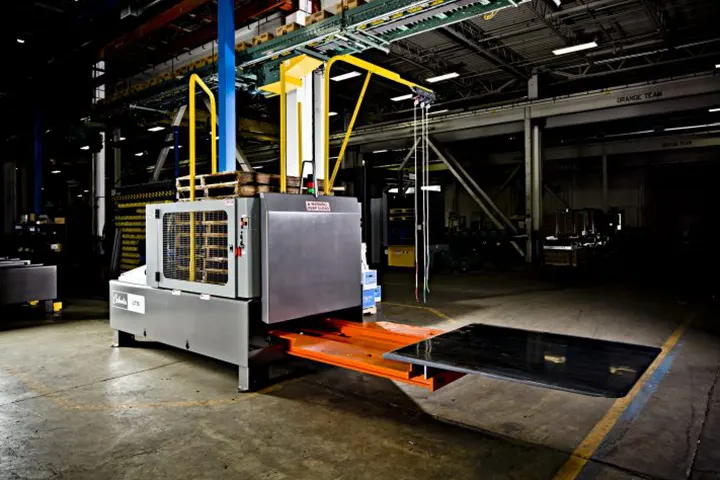
Compact palletizing solution designed for moderate-speed production lines requiring efficient floor space utilization.

QUESTIONS? CALL +91 72289 31741

2

FL1000-SW

Advanced configuration featuring improved product handling flexibility and optimized layer transfer functionality.

QUESTIONS? CALL +91 72289 31741

3

Integrated Bagging & Palletizing Systems

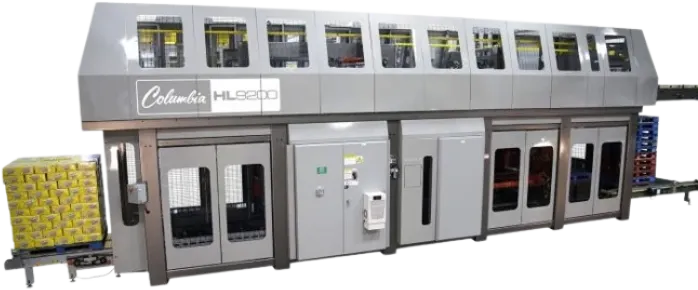
FL2000

High-reliability floor level palletizer machine designed for medium to high-capacity manufacturing operations.

QUESTIONS? CALL +91 72289 31741

4

FL2500

Enhanced throughput system offering improved stacking stability and faster pallet formation cycles.

QUESTIONS? CALL +91 72289 31741

5

FL3000

Heavy-duty industrial floor level palletizer engineered for continuous high-volume industrial palletizing applications. Features include automatic pallet dispensing, smart layer alignment systems, modular layouts, and integrated safety circuits.

QUESTIONS? CALL +91 72289 31741

Main Characteristics of Floor Level Palletizer

Our floor level palletizer equipment is designed to deliver steady performance in harsh industrial settings. Besides, it also focuses on the ease of use, safety, and the right conjunction of flexibility with an ergonomic infeed height of approximately 914 mm.

01

Infeed Height

Approximately 914 mm to ensure safe, comfortable, and ergonomic access during operation and maintenance.

02

Fast Case Handling

Capable of processing up to 40 cases per minute (pattern dependent) to ensure efficient, high-throughput productivity.

03

Multi-Format Packaging Compatibility

cartons, shrink-wrapped packs, trays, bags and pails can easily be handled.

04

Simple Touchscreen Interface

Intuitive HMI makes it super easy to select the patterns, monitor operations, and run diagnostics.

05

Flexible Modular Design

Gives different layout and space constraint configurations for installations.

06

Enhanced Safety & Durability

Category 3 safety systems and rugged construction suitable for 24/7 industrial operations are included.

How Floor-Level Palletizers Work

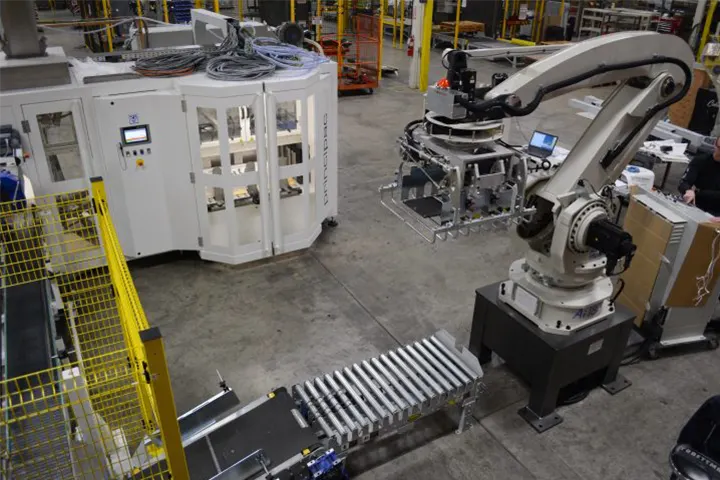
A floor level automatic palletizer uses a ground-level conveyor to bring in products, form them into layers, and stack them onto pallets, all automatically in a continuous cycle. After finishing, the pallet is discharged for wrapping or other handling, and the machine also supports custom patterns and integration with other systems.

Why Choose Us for Floor Level Palletizing Solutions

As a globally recognized floor level palletizer supplier, Columbia Machine India combines international engineering expertise with localized manufacturing support to deliver high-performance automation systems for Indian and global industries.
Floor level
01
Global Technology Leadership
Part of Columbia Machine Inc., serving industries across more than 100 countries worldwide.
Customized palletizing systems tailored to application-specific production requirements.
Engineered for demanding industrial operations with high throughput and stable load formation.
From conveyors and pallet dispensers to robotic integration and wrapping systems.
Comprehensive installation, commissioning, spare parts, training, and maintenance assistance.
Designed to reduce operational costs while improving manufacturing productivity and pallet handling efficiency.

Streamline‍‌‍‍‌‍‌‍‍‌ Your Palletizing Operations by Ground-Level Efficiency

Contact a reputable manufacturer of floor-level palletizer in India for a tailor-made solution and enhance your productivity by investing in a cost-effective palletizing solution.

Palletizing Solutions for Every Industry

From food and beverages to healthcare, logistics, e-commerce, automotive, electronics, and more, our palletizing solutions are designed to meet the diverse handling and production requirements of modern industries.

FAQs

What is the advantage of a floor level palletizer?

A floor level palletizer simplifies installation, reduces infrastructure costs, improves accessibility, and enhances operator safety compared to elevated palletizing systems.

Yes, an automatic floor level palletizer performs product handling, layer formation, pallet stacking, and load discharge with minimal human intervention.

Yes, the system supports cartons, bags, trays, bundles, shrink-wrapped products, and multiple industrial packaging formats.

Industries including FMCG, beverage, food processing, chemicals, warehousing, personal care and pharmaceuticals commonly use these systems.

Columbia Machine India offers fully customized floor level palletizing systems designed according to production throughput, layout, and application requirements.

Absolutely. Reduced labor dependency, low maintenance requirements, and efficient operation make it a highly cost effective palletizing solution for modern manufacturing facilities

Copy link
Please enable JavaScript in your browser to complete this form.