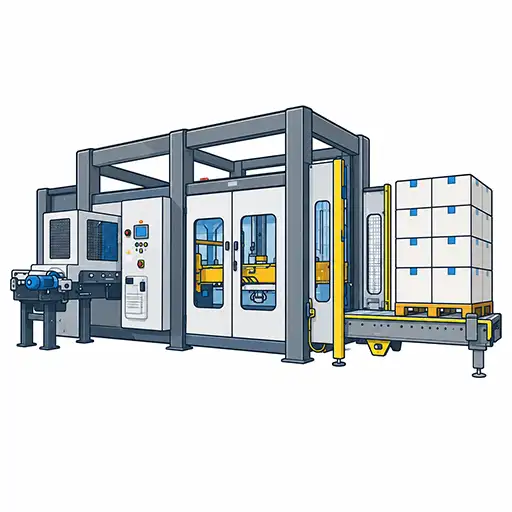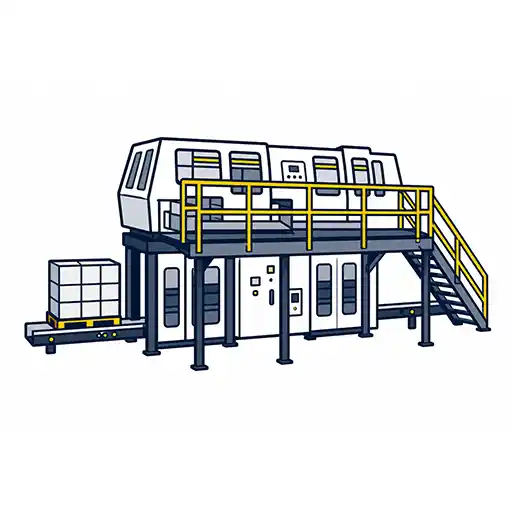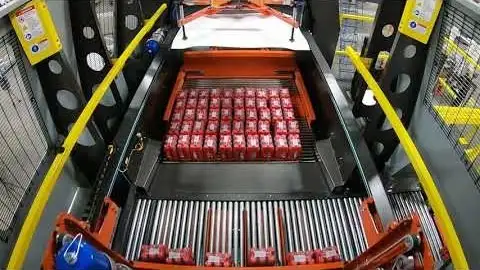
Revamps vertical product flow to make the accumulation process faster, allowing more accurate product handling and even palletizing operations.
Through smart row making and programmed layer sequencing, the software makes pallet designs that are not only stable but also optimized.
Delivers consistent, gentle, layer positioning with less product shifting and better pallet stability.
Brings together PLC-operated controls, live system monitoring, and conveyor communication in a coordinated manner to realize the highest level of operational performance.
It is a must for production facilities with vast volume to have a high-speed automation, uninterrupted material flow, and accuracy-controlled palletizing in order to get the highest level of operational efficiency. High-Level Palletizers are equipped with intelligent automation systems to increase throughput, load accuracy, and production reliability.
Allows for continuous palletizing with fewer cycle times and maximum production output.
Points to the use of the servo-driven system for the correct positioning of the product and the loading of the transfer.
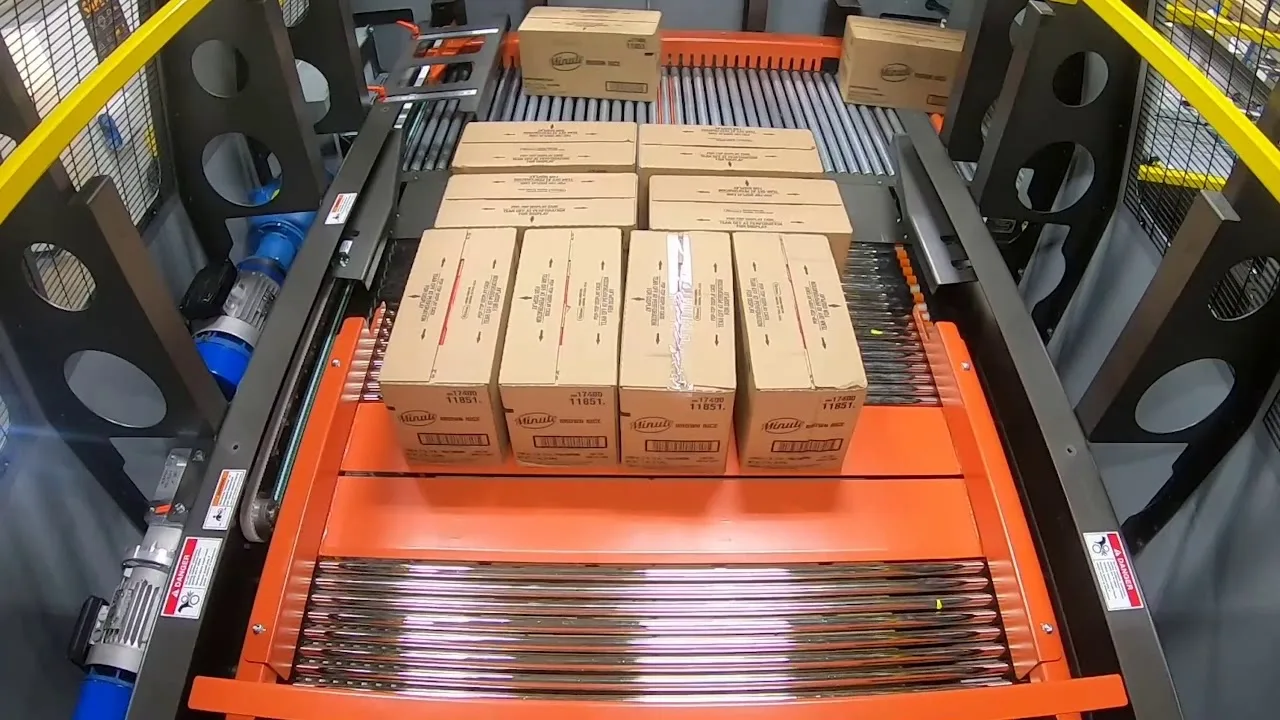
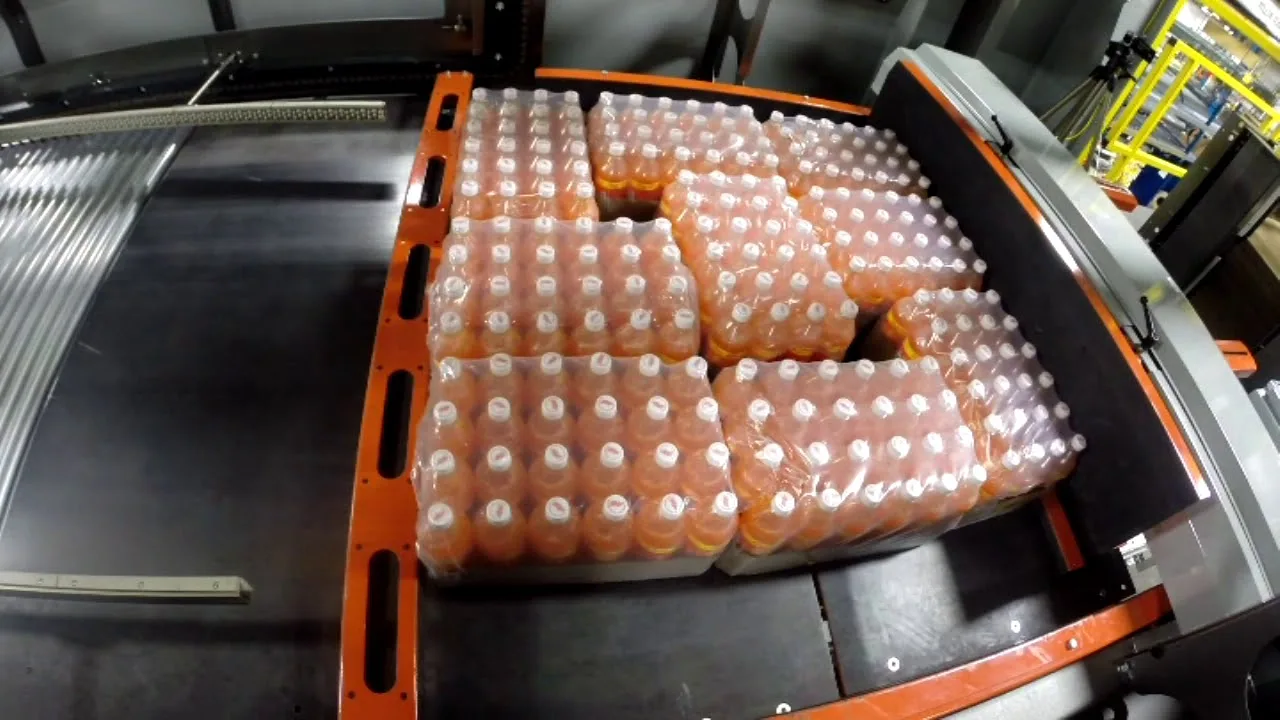
Maintains stable pallet patterns via automated row forming and load alignment.
Is capable of real-time monitoring, diagnostics, and smooth production line synchronization.
The process is done with a minimum of manual handling, thereby enhancing safety at the workplace and process consistency.
Provides a flexible automation architecture for Industry 4.0 production environment expansion.
These palletizing systems can operate at a very high pace and can handle a large number of products, yet the flow of materials remains uninterrupted.
The integrated mechanical components that automate the squaring of layers and row alignment, as well as performing the compression, make sure that pallet dimensions are uniform and load stability of the structure is excellent.
Layer placement control using high-speed servo control systems that reduce vibration results in improved accuracy of position and less product displacement.
It enables smart changes in machine settings for handling different types of packaging, such as bags, cartons, crates, bundles, and even mixed packaging, with very few production stops.
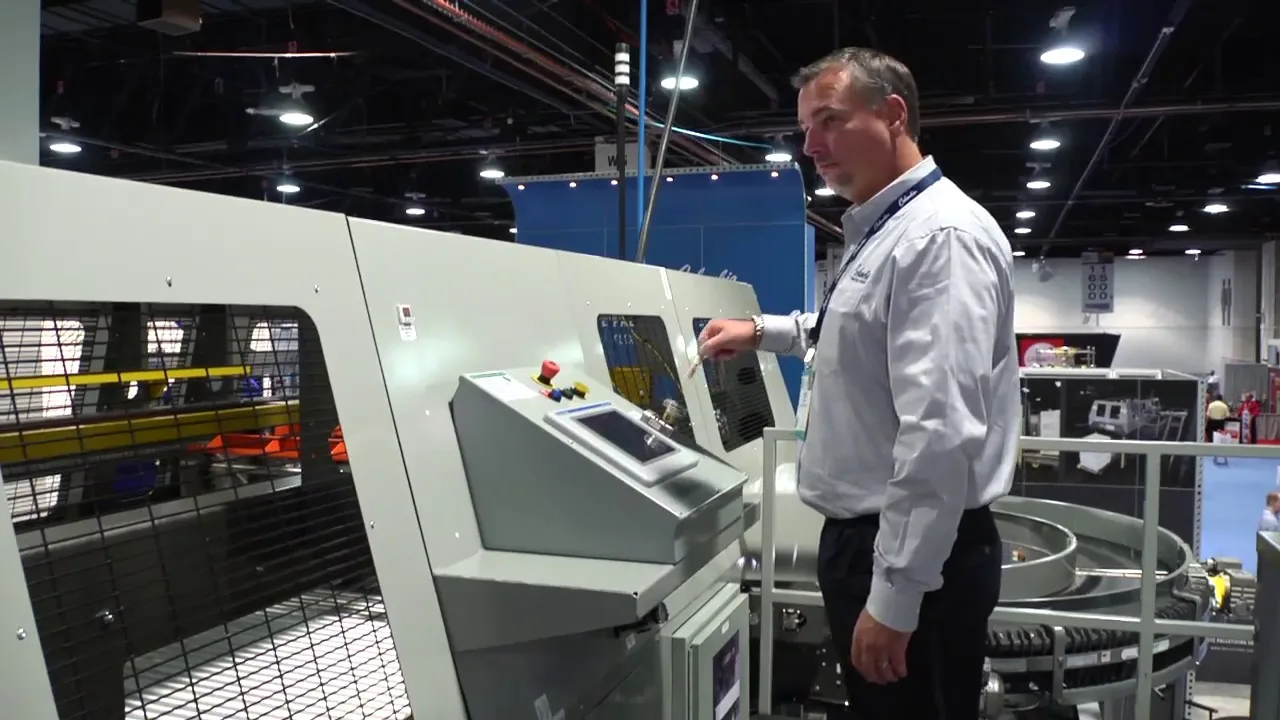
PLC-HMI design that includes not only real-time diagnostic features, but also conveyor synchronization and automated fault detection that significantly improve visibility and operational control.
Using an industrial-grade framework structure along with strengthened mechanical components and transfer systems characterized that the equipment will function reliably over a long period of time even in 24/7 production scenarios.
Offering technologies like smart sequence, different patterns and user-friendly control interfaces.
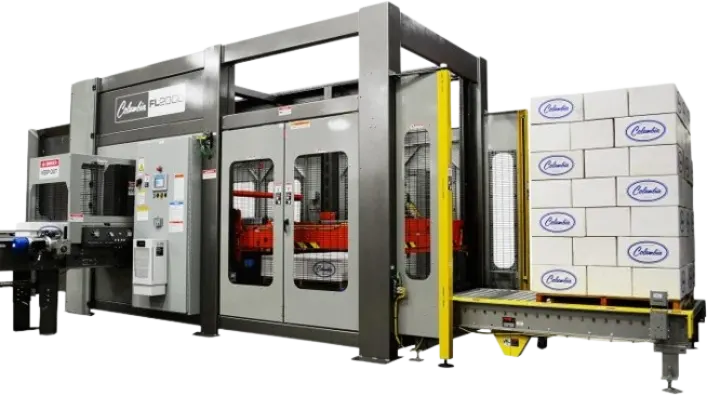
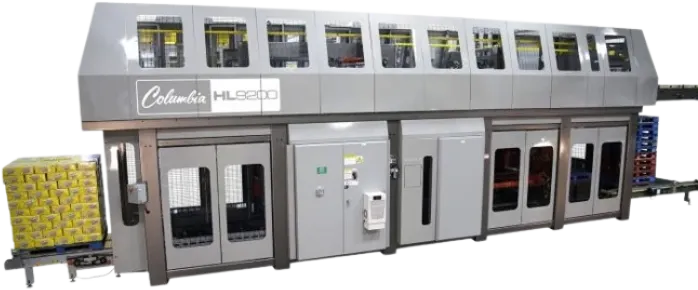
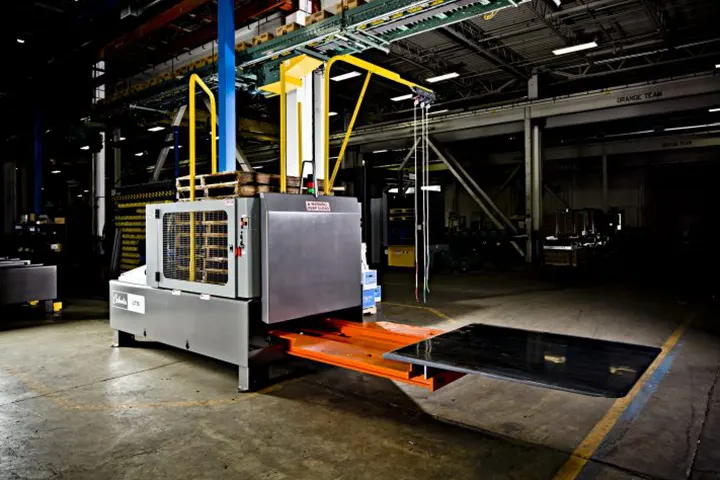
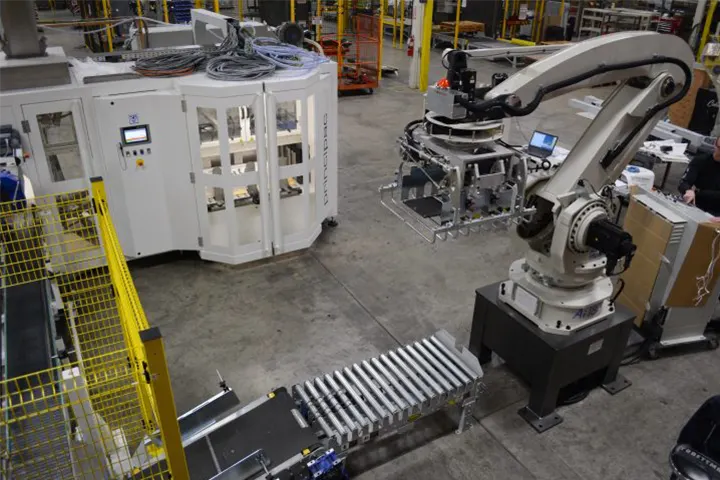
Generally, a high-level palletizer is a machine that automatically stacks items onto pallets at a very high speed. This significantly changes the whole scene of manufacturers by reducing the time spent on manual tasks of palletizing and also ensuring a uniform layer forming of products.
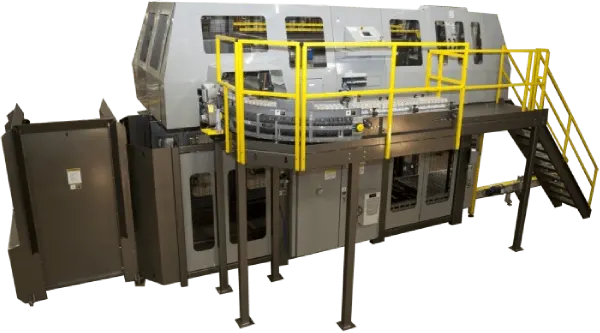
Most importantly, what differentiates a high-level palletizer from a floor-level one is that the high-level has the capability to use an elevated infeed design, allowing not only quicker product handling but also more efficient stacking.
In fact, industrial high-level palletizers are highly versatile and widely used across industries such as FMCG, food processing, chemicals, and many more for efficient and automated palletizing operations.
Basically, a cost-effective palletizing solution comes down to the major factors such as throughput capacity, automation level, and customization required.
Yes, it can. Using a high-level palletizing system is efficient for handling different types of products such as bags, cartons, crates, and other packaging formats.
Indeed, a very large number of automatic high-level palletizers are fully automatic and require very little human intervention while providing consistent performance.